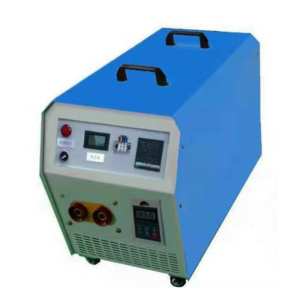
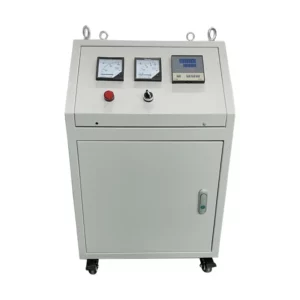
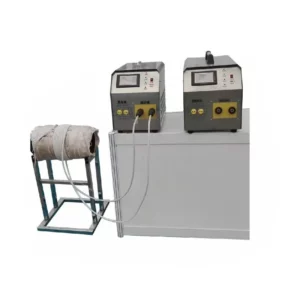
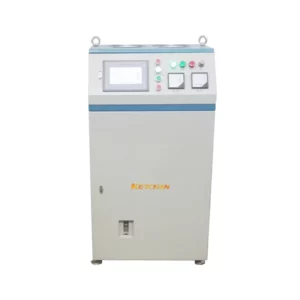
Induction heating is highly effective for correcting steel welds, particularly in addressing welding distortions and residual stresses. Here’s how it works:
- Preheating: The area around the weld is preheated using induction heating to a specific temperature. This helps in reducing the cooling rate of the weld puddle and minimizes the risk of cold cracking.
- Stress Relief: Post-weld heat treatment (PWHT) relieves residual stresses in the weld and heat-affected zone. This improves the toughness and reduces the risk of brittle fracture.
- Distortion Correction: Localized heating is used to correct distortions by creating high local stresses that pull the component back into shape as it cools.
Induction heating offers several benefits, including greater consistency in heating, faster time to temperature, ease of use, and improved safety compared to traditional methods.
Thermal correction of rail welds
Stress relief heat treatment of pipeline welds after welding
Preheating of straight welds of bridge steel plates, thickness 30 90mm, 260℃
Preheating of pipe girth weld, 300℃
Preheating of fillet welds of railway bridge steel structures, temperature 120℃
Induction preheating of steel plates before welding
Induction heating belt arrangement for steel structure welding preheating
Weld correction and heat treatment of steel structures
Mobile induction heating for welding seam correction of ships and steel structures
Mobile induction heater for welding seam correction of ships and steel structures (2)
Mobile induction heater for welding seam correction of ships and steel structures (1)
Mobile induction heater for heat treatment of ship plates and steel structure welds (2)
Mobile induction heater for heat treatment of ship plates and steel structure welds (1)
Ship Plate Weld Correction2
Ship Plate Weld Correction1